You are here:
Why Automatic Riveting Equipment Demand Keeps Growing - Sheet Metal
China is one of the world's largest markets for industrial automatic control systems and equipment. Demand for automation hardware from traditional plant retrofits, factory automation programs and enterprise digitization has stayed strong for years, and control technology is moving quickly toward intelligence, networking and integration. Down on the riveting line, demand for automatic riveting equipment such as auto-feed blind rivet machines, pneumatic rivet nut guns and pneumatic rivet guns has grown visibly over the past few years. This article skips the buzzwords and answers what manufacturers actually ask: what is driving demand, which riveting operations should be automated first, and whether your plant should buy now.
Sheet metal plants care about cycle time and uptime, and the pneumatic line is built around both. Everything below applies to auto-feed blind rivet machine work in that shop-floor setting.
What sheet metal and enclosure plants should remember: four forces driving demand for automatic riveting equipment; which riveting operations get automated first; the typical path of an automation upgrade; how to decide whether to buy now.
1. Four Forces Driving Demand for Automatic Riveting Equipment
| Driver | What it changes on the riveting line |
|---|---|
| Rising labor cost and hard-to-fill openings | Blind rivet and rivet nut jobs are repetitive, dull and physically heavy, so younger workers avoid them; a labor shortage in peak season goes straight to delivery dates |
| Tighter quality consistency requirements | Manual riveting depends on feel and fatigue, so missed rivets, proud rivets and thread stripping vary widely; customers in automotive and data centers now demand batch-level consistency and traceability |
| High-mix, low-volume production as the new normal | Faster product turnover and frequent changeovers mean the equipment must switch sizes quickly and run several rivet and nut types instead of one dedicated product |
| Downstream industries expanding | New energy vehicles, energy storage, data center cabinets, EV charging piles and home appliances keep adding capacity, and those thin-sheet assemblies carry many fastening points, so demand for automatic riveting equipment scales with them |
2. Which Riveting Operations Get Automated First
Automation follows a clear priority order: the first stations to be automated are those with many fastening points, a tight cycle and a repeatable motion. Take a cabinet door and frame line with a hundred rivet points, server chassis shelf assembly, an appliance shell line or an automotive parts line: operators there pick up a rivet, line it up and pull the trigger all day, and that is exactly where fatigue sets in and rivets get missed, so the return is highest. The opposite holds for rework and prototype stations with scattered points, a few dozen parts per batch and constant size changes; those are better served by pneumatic semi-automatic tools. For a way to judge the fit, see why factories move to custom automatic riveting equipment.
Most sheet metal plants change rivet sizes more often than they change machines.
3. The Typical Path of an Automation Upgrade
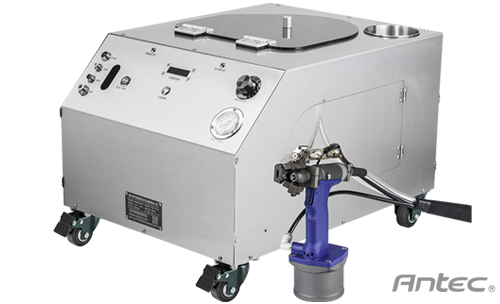
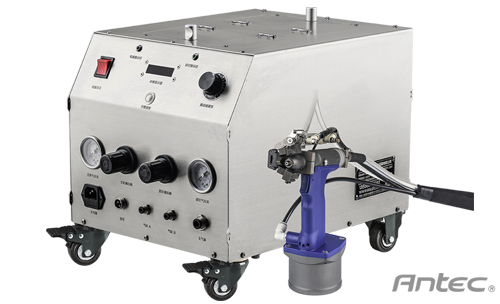
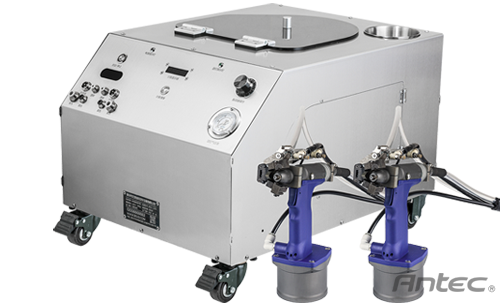
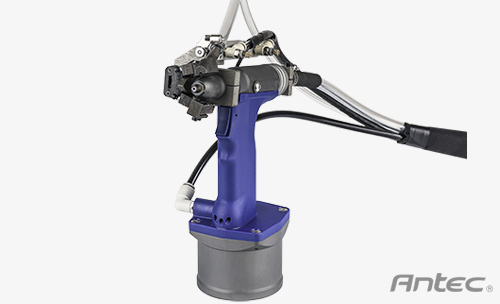
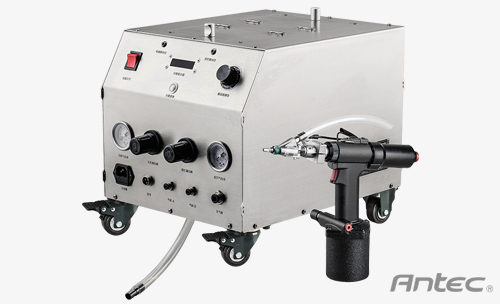
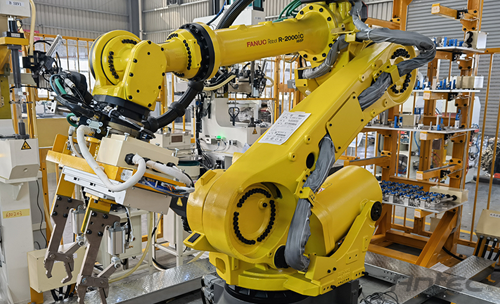
Most companies climb three levels. The first is the pneumatic semi-automatic tool, which takes the hand force out of the job but still needs a rivet placed by hand. The second is handheld auto-feed equipment: an auto-feed blind rivet machine or an pneumatic rivet nut gun sorts fasteners in a bowl feeder and blow-feeds them to the gun, so the operator only pulls the trigger; one machine typically absorbs the repetitive work of about three operators and can raise output up to about three times over manual work. The third is a fixed dedicated machine or a robotic cell for a dedicated line with fixed points and the tightest cycle, which can be tied into the line controls. Nobody has to jump to level three: most plants pilot at their busiest station, verify with real data, then roll out. For a comparison of machine types, see handheld, fixed, dual-gun and robotic cells compared.
4. How to Decide Whether to Buy Now
Check four numbers. First, how many people work the riveting stations and what they cost per year. Second, how many rivet or nut points go into one unit and what your annual output is. Third, what share of your rework and scrap comes from missed rivets and stripped threads. Fourth, how often peak season leaves you short of people and late on delivery. When a station runs full shifts, needs several operators on rotation and its defects trace back to hand work, automatic equipment usually pays back in 2-6 months. The safest way to settle it is not to trust a demo speed figure: have the supplier bring the machine to your plant and run a continuous sample with your own parts and rivets, measuring cycle time, jam rate and pass rate on site. Trial policy: is there a free trial of an auto-feed blind rivet machine. Antec has focused on auto-feed blind rivet machines, pneumatic rivet nut guns and pneumatic rivet guns for 16 years, serving 800+ enterprises and delivering 3,296+ automatic riveting solutions.
Commissioning on site is where the feed rate and the fixture get matched to the panel.
Industry Trend FAQ
Practical Q&A
The core case for automation is labor and defect cost, not industry growth. When orders are volatile, handheld auto-feed equipment is the better choice because it keeps you flexible: no labor shortage in peak season, no idle machine in the slow months.
What gets replaced is the repeated pick-up-and-trigger motion. Operators move to loading, inspection and tending several machines; the skill level rises, the physical load falls, and retention usually improves.
If you have many fastening points and two or more people working at them full time, it is worth an evaluation. With only a few points, stay on pneumatic semi-automatic tools for now, standardize your sizes and process, then upgrade.
The supplier can arrange an on-site sample run, or you can book a visit to the Huizhou manufacturing base to see the plant and a continuous running test.
The main structure is built for a long service life. The pull rod, nosepiece and seals are wear parts and can be replaced, so with scheduled maintenance the machine runs reliably for years. For maintenance requirements, see auto-feed blind rivet machine operation and maintenance guide.
Auto-Feed Blind Rivet Machine at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
Bring a sample panel to the trial - the engineer will set the feed and the nosepiece on the spot.
Standard factory work, mainstream pneumatic equipment
Tell us the rivet range and the output target. We will confirm the model, the 50-60 rivets per minute rating, the parts supply and the on-site commissioning.
Further reading: how fast is an auto-feed blind rivet machine: cycle time and output calculation · how to choose an auto-feed blind rivet machine manufacturer · auto-feed blind rivet machine selection advice
 Previous