You are here:
Pneumatic Rivet Nut Gun Selection Guide: Appliances, Cabinets
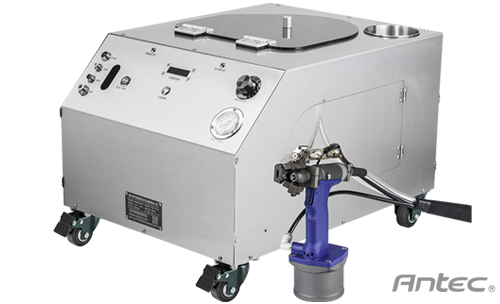
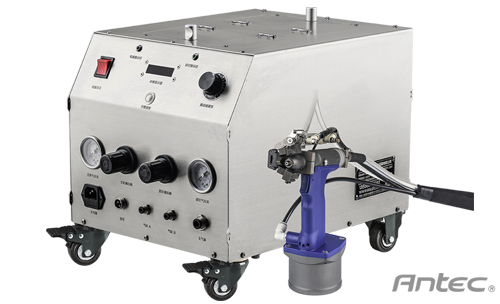
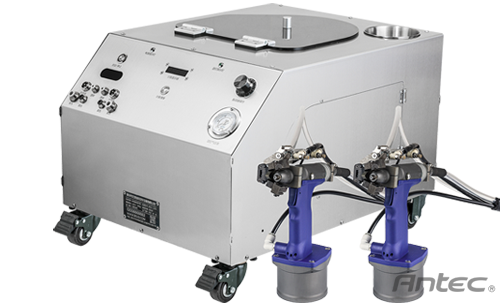
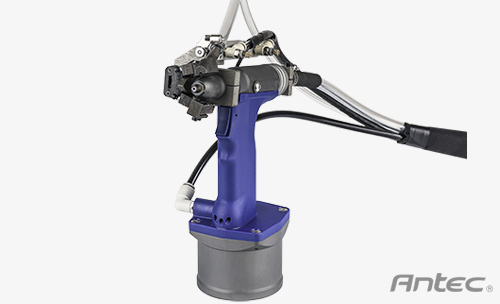
Appliance, electrical cabinet, and new energy manufacturers often need removable internal threads in thin sheet, aluminum extrusions, and powder-coated panels. For that job the right tool is an pneumatic rivet nut gun, not a standard auto-feed blind rivet machine. This guide covers selection for three production environments: home appliances, electrical cabinets, and new energy battery assembly.
For cabinets, chassis and enclosures, an auto-feed machine and a pneumatic gun usually handle the whole rivet range at 50-60 rivets per minute. Everything below applies to pneumatic rivet nut gun work in that shop-floor setting.
For sheet metal and enclosure plants, the essentials: decide first whether a rivet nut is the right fastener; pneumatic rivet nut gun selection by workshop type; matching nut size to pull force; common mistakes.
1. Decide First Whether a Rivet Nut Is the Right Fastener
When the workpiece is thin sheet or aluminum extrusion, needs an internal thread, has to come apart and go back together repeatedly, and cannot tolerate weld distortion or stripped tapped threads, a rivet nut is the better process. It cold-forms an M3–M12 thread in one pass, leaves the back face undistorted, needs no tapping, and can be removed and reinstalled at will.
2. Pneumatic Rivet Nut Gun Selection by Workshop Type
| Workshop type | Typical workpieces | What to prioritize |
|---|---|---|
| Home appliances / kitchen | Door panels, brackets, removable panels | Handheld fast pneumatic rivet nut gun, scratch protection |
| Electrical cabinets | Cabinet doors, mounting plates, aluminum beams | Dual-motor high pull force, M5–M12 |
| New energy | Battery trays, PACK, energy storage cabinets | Robotic or gantry station, pull test for sealing |
For cabinets and chassis, a trial on your own panels settles more than a specification sheet.
3. Matching Nut Size to Pull Force
M3–M6 suits appliances and thin panels, M6–M10 suits cabinet doors and mounting plates, and M10–M12 suits aluminum extrusion beams, energy storage cabinets, and battery trays. For aluminum, specify knurled rivet nuts made for aluminum, and pull-test the thickest material at the trial before you commit to a size.
4. Common Mistakes
Mistake one is tapping aluminum directly and stripping the thread. Mistake two is running M10 or M12 nuts with a low-pull gun, so the nut never seats. Mistake three is repairing a powder-coated part by weld touch-up, which damages the finish. Book a free trial first to lock down nut sizes and hole positions. For cabinet work, see power distribution cabinets and electrical equipment; for battery and storage work, see new energy, lithium battery and energy storage.
Door panels and mounting plates had been tapped, and stripped threads drove constant rework. After switching to a dual-motor pneumatic rivet nut gun and building a size-and-hole position chart, the plant forms M5–M10 threads in one pass, can add nuts after powder coating, and cut thread work per cabinet by about one third.
Practical Q&A
Yes. The nut cold-forms into the prepunched hole with no welding and no damage to the coated surface, which makes it practical for field changes and rework.
Match the nut size and nosepiece to the material thickness and control stroke pressure. At the trial, run a panel from the same process and confirm no bulging or marking before you sign off.
Pneumatic Rivet Nut Gun at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
If the rivet size and sheet thickness are known, the team can name the model and the air requirements in one reply.
Standard factory work, mainstream pneumatic equipment
Tell us the rivet range and the output target. We will confirm the model, the 50-60 rivets per minute rating, the parts supply and the on-site commissioning.
 Previous