You are here:
Hot vs. Cold Riveting: Where the Pneumatic Rivet Nut Gun Fits
In riveting, hot and cold are two entirely different approaches. Customers choosing an pneumatic rivet nut gun or an auto-feed blind rivet machine ask the same question: should our part be hot riveted or cold riveted, and which camp do rivet nuts belong to? This article separates the two by principle, by equipment and by application, and explains why sheet metal shops, enclosure and cabinet builders and new-energy plants settle on cold riveting.
Pneumatic models are the mainstream choice in sheet metal shops: they cover the vast majority of standard riveting jobs and are simple to maintain. Everything below applies to pneumatic rivet nut gun work in that shop-floor setting.
For sheet metal and enclosure plants, the essentials: the core difference between hot and cold riveting; rivet nuts are cold riveting: where the pneumatic rivet nut gun fits; why thin sheet and automated lines choose cold riveting; the usual doubt: is cold riveting strong enough?.
1. The Core Difference Between Hot and Cold Riveting
| Compare | Hot riveting | Cold riveting |
|---|---|---|
| Forming principle | The rivet is heated to red heat and upset while the metal is soft and plastic | At room temperature, pull force or press force cold-forms the fastener |
| Heat required | Yes: a furnace, an induction coil or an electrically heated riveting tool | None; air, electric or hydraulic drive |
| Typical fasteners | Solid rivets and semi-tubular rivets, in large diameters and high-strength steel | Blind rivets, rivet nuts and clinch parts |
| Effect on the workpiece | A heat-affected zone that can distort, discolor or damage the coating | No heat distortion, so assembly can follow powder coating |
| Working method | Usually two-sided, with a bucking bar, in a hot environment | One-sided work, hand-held or automated |
| Typical applications | Bridges, vehicle chassis, heavy steel structures and large airframe parts | Enclosures and cabinets, sheet metal, appliances, auto parts and new energy |
2. Rivet Nuts Are Cold Riveting: Where the Pneumatic Rivet Nut Gun Fits
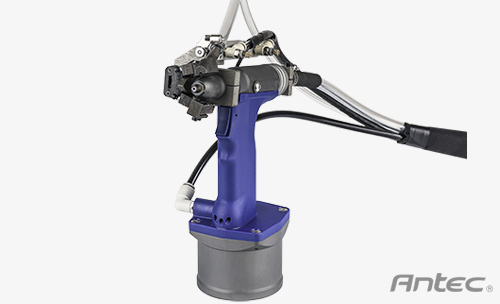
A pneumatic rivet nut gun pulls its mandrel axially at room temperature, so the nut body is cold-extruded into a bulge on the far side of the sheet. That is cold forming, the textbook cold riveting process, and a blind rivet that snaps its mandrel to form the head follows the same principle. Cold riveting generates no high temperature, so the sheet does not warp, anneal or discolor, which makes it the right choice for cosmetic parts that have already been painted, powder coated or anodized, and for aluminum and thin steel that conduct heat fast and distort easily.
Parts are held in stock because a stopped line costs more than the part.
3. Why Thin Sheet and Automated Lines Choose Cold Riveting
First, distortion stays under control: thin sheet warps at the slightest heat, while cold riveting delivers a stable forming force and a flat panel. Second, one side is enough: the back of an enclosure, a square tube or a closed chamber cannot be reached, so hot riveting with its bucking bar simply cannot work there, while one cold riveting gun can. Third, automation comes easily: a steady cycle, no waiting for heat, no open flame and no fume make cold riveting a natural fit for auto-feed equipment and robot cells on volume lines. Fourth, it is safer and cleaner: no high temperature, no welding smoke and no fire precautions, which means a better shop floor and less physical strain.
4. The Usual Doubt: Is Cold Riveting Strong Enough?
On a thin-sheet joint, reliability usually turns on fastener selection and forming quality rather than on hot versus cold. Structural blind rivets, and hex and knurled rivet nuts, are already used in volume on automotive and new-energy structural parts; their pull-out load and torque are tabulated by size and can be verified with a pull test on a sample. Hot riveting is genuinely required only for large-diameter, high-strength steel load-bearing joints such as heavy truck frames and bridges. Tell the supplier what the joint has to carry and select from pull-test data instead of the impression that hot must be stronger. For the types available, see rivet nut types compared.
On the shop floor, the air supply and the nosepiece fit decide whether the rated cycle time holds.
Hot vs. Cold Riveting FAQ
Shop-Floor Questions
No, and it does not need to. An pneumatic rivet nut gun is cold riveting equipment built around the cold forming of rivet nuts; hot riveting needs a heated riveting tong or a hot riveting machine.
Yes, and that is one of the advantages of cold riveting: assembly after coating does not damage the finish. Just hold the hole position and the gun angle to the process sheet.
The deformation is small and stays inside the nut, so the effect on the panel is limited. Standard aluminum sheet and profiles show no problems in long service, and critical load-bearing parts can be checked with a pull test.
The two fasteners use different gun heads and different forming principles, so the usual setup is one auto-feed blind rivet machine and one pneumatic rivet nut gun. A robot workstation can cover both processes by changing guns.
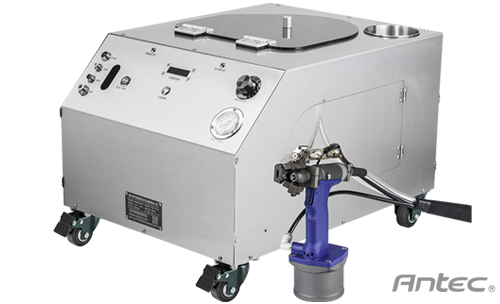
Pneumatic Rivet Nut Gun at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
Antec has served more than 800 sheet metal and enclosure plants with free trials, on-site commissioning, parts supply and maintenance.
Sheet metal plants: try it on your own panels
Send the rivet size and sheet thickness. We will match the auto-feed machine or the pneumatic gun, then run your panels on site before you decide.
5. Can a Product Designed for Hot Riveting Switch to Cold?
Plenty of traditional sheet metal parts and vehicle fittings were designed for hot riveting years ago. Converting them to cold takes three steps. Redesign the joint: replace solid rivets with blind rivets or rivet nuts, and prefer rivet nuts wherever a screw has to go in afterwards. Prove the strength: run pull, shear and vibration tests against the original joint requirement and let the data confirm the substitution. Review the line: cold riveting needs no heating station and no fume extraction, so the layout usually gets simpler. For products that are already thin sheet, reachable from one side and assembled after coating, moving to cold riveting usually pays off in both distortion control and automation; large-diameter high-strength steel load joints should stay hot riveted. On a mixed line, keep the two fastener families, their hole patterns and their tools separated so nothing is installed in the wrong place.
Cold riveting removes the furnace, the fume extraction and the heat-resistant tooling, and a hand-held unit is not expensive. Auto-feed machines and robot cells cost more, but against the labor and energy they save, a high-volume line usually pays back quickly. Run the numbers on your own part.
Further reading: pneumatic rivet nut gun: uses, working principle and common questions · blind rivet knowledge roundup · pneumatic rivet nut gun
 Previous