You are here:
EV Growth Drives Automatic Riveting Equipment for Auto Parts - Sheet Metal
The EV industry has been one of the fastest-growing downstream markets for automatic riveting equipment in recent years. Battery, motor and electronic control systems, together with lightweight bodies and interiors, generate heavy demand for joining thin sheet, aluminum extrusions and dissimilar materials, a mix that a single welding process can no longer cover. That is why auto-feed blind rivet machines and pneumatic rivet nut guns keep moving onto automotive parts lines, and why component makers in every major EV cluster are upgrading at the same time.
Pneumatic models are the mainstream choice in sheet metal shops: they cover the vast majority of standard riveting jobs and are simple to maintain. Everything below applies to auto-feed blind rivet machine work in that shop-floor setting.
For sheet metal and enclosure plants, the essentials: why EV production uses so much riveting; typical parts and fasteners; what automotive lines demand from automatic riveting equipment; upgrade advice for component plants.
1. Why EV Production Uses So Much Riveting
First, lightweighting: range pressure pushes bodies and structural parts toward aluminum alloy, high-strength steel sheet and extrusions, and where thin sheet distorts badly under welding, riveting forms the joint cold and leaves the panel flat. Second, heat-sensitive parts: welding heat is not allowed near a battery pack or a control box, and blind rivets and rivet nuts are cold connections with no thermal distortion. Third, dissimilar materials: aluminum to steel, or aluminum to composite, cannot be welded conventionally, so mechanical fastening is the more reliable route. Fourth, assembly after coating: riveting runs after e-coating or paint without breaking the surface treatment.
2. Typical Parts and Fasteners
| Part | Joining Requirement | Typical Process / Equipment |
|---|---|---|
| Battery pack / tray | Aluminum frame, base plate and bracket joints, with high consistency | Structural blind rivets, auto-feed blind rivet machine or robotic cell |
| Control / e-drive housing | Threaded inserts in thin sheet, grounding, accessory mounting | Rivet nuts, pneumatic rivet nut gun |
| Interior and instrument panel frame | Many fastening points, tight cycle time, visible surfaces | Auto-feed blind riveting, fixed dedicated machine |
| Bumper / bracket | Thin-wall parts, no press marks | Automatic blind riveting equipment with a matched nosepiece |
| Charging-related structural parts | Corrosion resistance, outdoor reliability | Stainless steel rivets / blind (closed-end) rivet nuts |
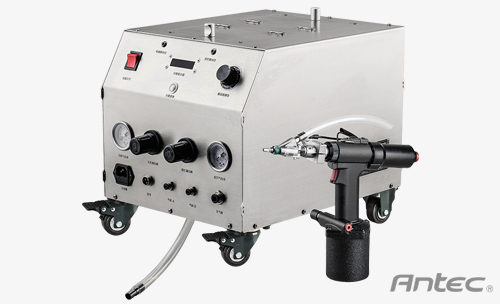
Parts are held in stock because a stopped line costs more than the part.
3. What Automotive Lines Demand from Automatic Riveting Equipment
Automotive work holds riveting equipment to a much higher standard than general sheet metal fabrication. Cycle time has to be stable enough to plan capacity backward from. Every joint needs identical parameters, and critical points need counting, missing-rivet detection and error proofing. The machine must tie into the line through part-present signals, interlocks and data logging. Model changeovers must be fast, with quick swaps of the feed track, nosepiece and program. And reliability has to hold over continuous running: Antec equipment is validated to a standard of 30,000 consecutive rivets without a jam, with an overall failure rate of about 0.3%. For a worked example see this EV component riveting case, and for more applications in the sector see new energy and lithium-battery energy-storage riveting solutions.
4. Upgrade Advice for Component Plants
Step one is to list the rivet and rivet nut specs and the per-point cycle time across every model, then consolidate specs first. Step two is to pilot an auto-feed machine or a fixed dedicated machine at the bottleneck station of a volume model and use a month of data to prove cycle time and defect rate. Step three is to copy the setup to similar stations and, at the new-model design stage, lock in hole positions and spacing to suit automation. For a mixed-model line, start with a handheld auto-feed gun and locating fixtures; reserve robotic cells for dedicated lines and high-volume fixed points. For a comparison of machine types see what types of auto-feed blind rivet machines are available.
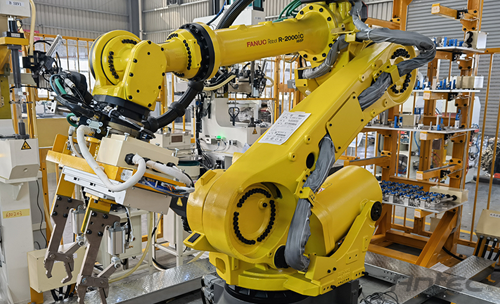
On the shop floor, the air supply and the nosepiece fit decide whether the rated cycle time holds.
EV Riveting FAQ
Shop-Floor Questions
Structural blind rivets and hexagonal rivet nuts are already used in volume on battery packs and body structures. Strength is read from the specification tables and verified by pull-out, shear and vibration testing, with test data governing every critical point.
Yes. Mechanical riveting does not depend on weldability, and joining dissimilar materials is one of the advantages riveting holds over welding. Match the fastener material to prevent galvanic corrosion.
Fixed dedicated machines and robotic cells can supply part-present, count and alarm signals to the line. Handheld tools generally cover counting and error proofing only. Raise the requirement during the solution stage.
Yes. The manufacturer serves every major automotive cluster and will bring a matched machine to your plant to run your own workpieces and measure cycle time.
Bring the equipment maker in at the process design stage, so hole positions and fastener selection are settled together. Changing holes and fixtures after volume production starts is pure waste.
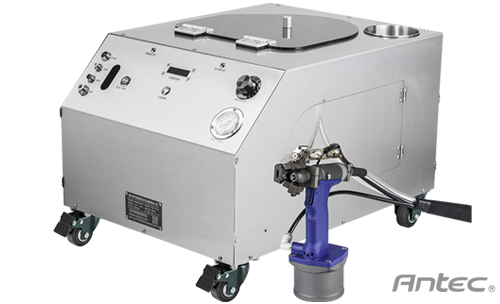
Auto-Feed Blind Rivet Machine at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
Antec has served more than 800 sheet metal and enclosure plants with free trials, on-site commissioning, parts supply and maintenance.
Sheet metal plants: try it on your own panels
Send the rivet size and sheet thickness. We will match the auto-feed machine or the pneumatic gun, then run your panels on site before you decide.
5. Global Support for Automotive Parts Manufacturers
Automotive clusters worldwide are dense with vehicle makers and their parts suppliers. Because the industry launches many models and validates on tight schedules, the manufacturer supports the whole cycle: it reviews the joining process from your parts and CAD data, brings a matched machine to run samples on site, and measures cycle time, forming quality and continuous stability on the spot. After commissioning it handles installation, operation training and first-article production support, and keeps a factory-direct supply channel for wear parts such as mandrels and nosepieces so lines do not wait. Component plants can bring the equipment maker in while quoting a new project, so hole positions, fastener specs and automation accessibility go into the process design together and no one reworks holes and fixtures after launch. For a worked example see this EV component riveting case.
Further reading: automatic vs. standard pneumatic rivet nut guns · EV component riveting case · auto-feed blind rivet machines
 Previous