You are here:
Automatic Riveting Equipment for High-Mix Sheet Metal Shops - Sheet Metal
Sheet metal shops are defined by high mix, low volume and tight delivery dates: cabinets, doors, mounting plates, aluminum panels and equipment enclosures rotate through the line, and the blind rivets and rivet nuts behind them come in too many sizes across too many hole positions. Whether a plant like this can run automatic riveting equipment at all, and how to bring it in without wasting money, is the question sheet metal plant owners care about most. This article lays out a gradual path that a large number of sheet metal plants have already proven.
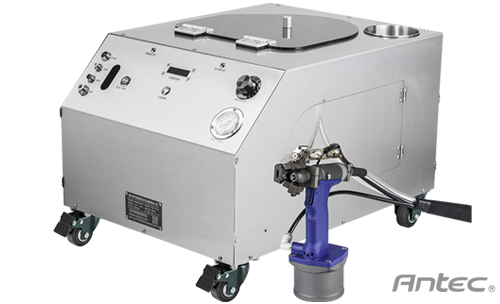
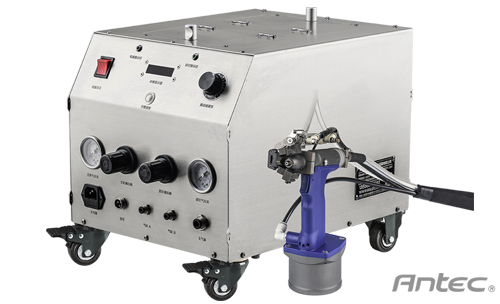
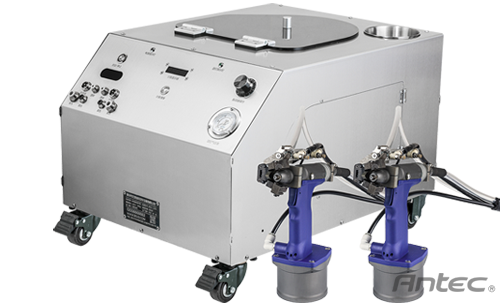
For cabinets, chassis and enclosures, an auto-feed machine and a pneumatic gun usually handle the whole rivet range at 50-60 rivets per minute. Everything below applies to auto-feed blind rivet machine work in that shop-floor setting.
What sheet metal and enclosure plants should remember: first, judge whether your plant is a fit; step one: consolidate fastener sizes before you buy anything; step two: lead with handheld auto-feed; step three: fixtures, then dedicated automatic riveting equipment.
1. First, Judge Whether Your Plant Is a Fit
| Plant profile | Recommendation |
|---|---|
| Dedicated blind rivet or rivet nut stations, with two or more operators working full shifts | Start with handheld auto-feed equipment |
| High volume on standard products such as standard cabinets, with fixed hole positions | Combine handheld tools with fixed dedicated machines |
| Batches of a few dozen parts, with sizes changing every day | Consolidate fastener sizes first, then add handheld equipment |
| Mostly rework, prototypes and one-off parts | Keep pneumatic semi-automatic tools |
2. Step One: Consolidate Fastener Sizes Before You Buy Anything
The biggest obstacle in sheet metal automation is not the equipment; it is fastener sprawl. One plant may run a dozen rivet and nut sizes, none of them in volume, and changeover time eats the savings. The first step is to audit the fastener list across every product and merge similar sizes, for example by standardizing on the M5 and M6 nuts you actually use and on two or three rivet diameters, then to standardize hole positions and hole diameters in the sheet metal process sheet. Once sizes are consolidated, the feed tracks, nosepiece variants and changeovers the automatic riveting equipment needs all fall sharply, and the payback improves right away. For the size range one machine can cover, see can an auto-feed blind rivet machine run every rivet size.
Most sheet metal plants change rivet sizes more often than they change machines.
3. Step Two: Lead with Handheld Auto-Feed
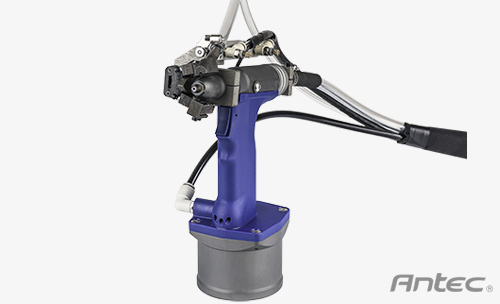
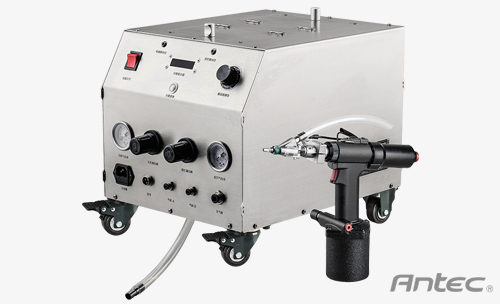
The best starting point for high-mix, low-volume work is a handheld auto-feed blind rivet machine or pneumatic rivet nut gun: a vibratory bowl feeder sorts the fasteners, a feed tube carries each one to the gun, and the operator only has to line up the nosepiece and pull the trigger. Tooling is not tied to one product, so any part shape works, and a size change means swapping a nosepiece and a feed track. Because the tool is not dedicated to a single part number, utilization stays high. Bowl feeders and feed mechanisms do demand consistent fastener dimensions, so buy standard rivets and nuts from a qualified supplier: burrs and deformed parts cause jams. For how feeding works, see how an auto-feed blind rivet machine feeds rivets and clears jams.

4. Step Three: Fixtures, Then Dedicated Automatic Riveting Equipment
Once a few product families such as standard door panels or mounting plates have steady orders, build locating fixtures for them. The part drops into place, the holes line up on their own, angled rivets disappear and the physical effort drops. As volume grows further, move to a fixed dedicated machine that locks in the hole pattern and the cycle time. A robotic cell makes sense only for a dedicated line with stable sizes and enough volume; there is no need to jump there in one step. That sequence (consolidate sizes, go handheld, add fixtures, then dedicate or robotize) splits the investment into small steps, and each step is funded by real data from the one before it.
Commissioning on site is where the feed rate and the fixture get matched to the panel.
5. How to Work Out the Payback
Run the annual numbers on four lines: labor at the riveting stations, including recruiting and turnover cost; rework and scrap from missed rivets and proud rivets; the extra output a faster cycle brings; and shop-floor management overhead. One handheld auto-feed machine usually absorbs the repetitive work of about three operators, and busy high-volume stations typically pay it back in 2-6 months. High-mix plants take somewhat longer, but the machine is versatile, so it never runs out of work. For how the price is put together, see how much does an auto-feed blind rivet machine cost, and for the full checklist before you buy, see what to check before buying an auto-feed blind rivet machine.
Sheet Metal Retrofit FAQ
Practical Q&A
Yes. A handheld auto-feed gun does not care what the part looks like. The key is to consolidate rivet and nut sizes down to a few, so you are not swapping feed tracks all day.
Swapping the nosepiece and the feed track is normally quick; the exact time depends on the machine model, so give the supplier your full size list during the purchase process and ask for a changeover plan.
The handheld gun travels to the part, which suits irregular and large workpieces better than a dedicated machine; fixed installations are for regular flat panels.
Start with one machine at your busiest station, run it for a month and confirm the real labor savings before adding more. That is the lowest-risk sequence.
The supplier can come to your plant and run a sample with your own parts and rivets, then measure time per rivet, jam rate and changeover time.
Auto-Feed Blind Rivet Machine at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
If the rivet size and sheet thickness are known, the team can name the model and the air requirements in one reply.
Standard factory work, mainstream pneumatic equipment
Tell us the rivet range and the output target. We will confirm the model, the 50-60 rivets per minute rating, the parts supply and the on-site commissioning.
6. The Management Basics That Keep the Machine Productive
The machine is only the foundation. To turn it into steady savings, a sheet metal plant needs three management basics. First, formalize the pre-shift check and the first-article confirmation: check air pressure, feeding and nosepiece condition every shift, and always run a first article after a changeover. Second, store fasteners by size in labeled bins, keep the qualified supplier fixed, and keep burred or deformed parts out of the bowl feeder. Third, write the hole diameter, hole edge distance and material thickness range into the sheet metal process sheet, so laser cutting and turret punching deliver consistent incoming parts. After a month or two, review the numbers: hours actually saved, jam rate, and which station is still the bottleneck. That review tells you whether the next step is another machine or a fixture and a dedicated unit. For day-to-day troubleshooting, see auto-feed blind rivet machine operation and maintenance guide.
Further reading: pneumatic rivet nut gun applications in sheet metal fabrication · types of auto-feed blind rivet machines · auto-feed blind rivet machine
 Previous