You are here:
Automatic Riveting Equipment for Home Appliance Production Lines - Sheet Metal
Home appliances are a classic high-volume, assembly-line industry. Air conditioners, washing machines, microwaves, range hoods, water heaters and small appliances all carry a large number of rivet and rivet nut points across their metal shells, internal brackets, doors and reinforcements. As labor costs rise and line takt times tighten, more and more appliance makers are replacing hand-held riveting with automatic riveting equipment that feeds and sets rivets on its own.
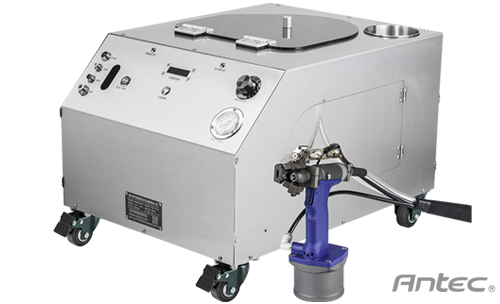
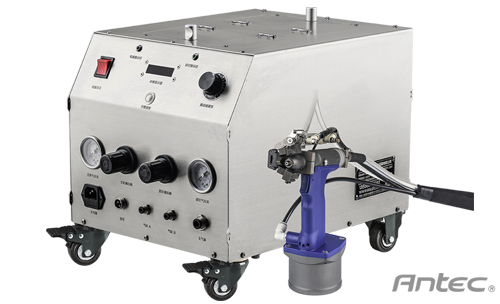
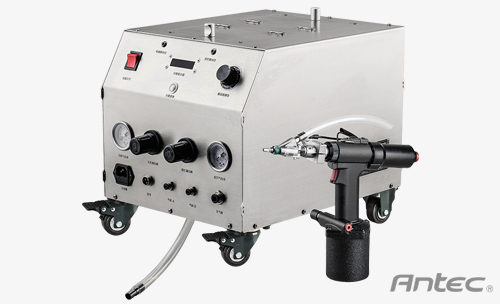
Pneumatic models are the mainstream choice in sheet metal shops: they cover the vast majority of standard riveting jobs and are simple to maintain. Everything below applies to auto-feed blind rivet machine work in that shop-floor setting.
In short, for sheet metal and enclosure plants: what makes appliance riveting different; typical products and rivet locations; automation options and the payoff; implementation advice.
1. What Makes Appliance Riveting Different
First, many thin-gauge cosmetic parts: 0.5-1.5mm cold-rolled steel, galvanized steel and aluminum, assembled after painting or film lamination, so press marks and scratches show. Second, fast takt times: the line runs to the second and the riveting station cannot become the bottleneck. Third, large batches and relatively stable models: high volume per model makes automation worthwhile. Fourth, quality shows up in after-sales: a loose door hinge or internal bracket turns straight into a warranty complaint, so consistency matters.
2. Typical Products and Rivet Locations
| Product | Typical rivet locations |
|---|---|
| Air conditioner (indoor / outdoor unit) | Shell, base pan, motor bracket, partition, valve bracket |
| Washing machine | Cabinet frame, door hinge reinforcement plate, counterweight and motor brackets |
| Microwave / oven | Cavity, shell, door, hinge and latch |
| Range hood | Housing, air duct, panel bracket, filter retainer |
| Water heater / small appliance | Tank hanger, shell, mounting back plate |
Pneumatic maintenance is simple, but it is not optional - water in the line is the usual culprit.
3. Automation Options and the Payoff
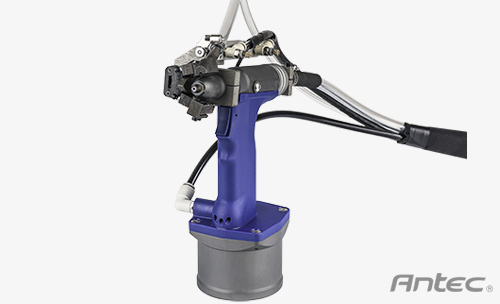
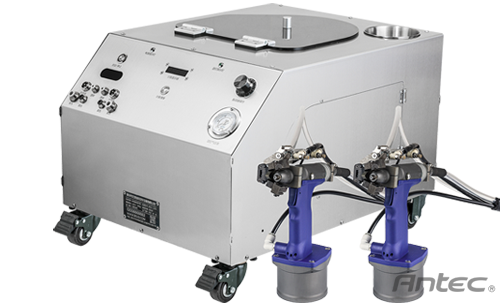
Appliance lines use three configurations depending on the station. At manual positions on the assembly line, a hand-held auto-feed blind rivet machine sorts rivets in a vibratory bowl, blows them to the nosepiece and sets them on the trigger pull, which removes the rivet pick-up motion; one machine usually takes over the repetitive work of about 3 workers and can raise output by up to 3 times compared with hand riveting. For regular parts such as doors and base pans, a fixed dedicated machine sets point after point automatically once the workpiece is in position, giving the steadiest cycle time. Symmetrical rivet patterns can run a dual-gun / dual-output setup that sets two rivets at the same time. On quality, rivet counting prevents misses and pull force stays consistent, so missed and unseated rivets and hinge-related after-sales issues drop noticeably. For the logic behind the upgrade, see why factories invest in custom automated riveting equipment.
4. Implementation Advice
First, pilot at the bottleneck station: count rivet points and cycle time at every station, then start with the one that runs at full load all day with the most people on it. Second, sample cosmetic parts first to confirm the nosepiece and pull force, so powder-coated surfaces come through without press marks. Third, plan alongside the line design and build machine suspension, feed hose routing and bowl placement into the station layout. Fourth, consolidate rivet sizes and standardize hole edge distances at the design stage of new models to reduce changeovers. Fifth, calculate payback from one month of output, labor and defect data at the pilot station; a typical high-volume line pays back in 2-6 months. Appliance makers can review the application options in the auto-feed blind rivet machine selection advice.
Parts are held in stock because a stopped line costs more than the part.
Appliance Industry FAQ
Shop-Floor Questions
Choose a matched nosepiece and pull force and hold the gun square to the surface, and cosmetic faces come out with no visible marks. Always run a cosmetic sample before full production.
Auto-feed gives a steady cycle (about 50-60 cycles/min as a reference figure for the rivet machine). The single- or dual-gun configuration is then set to your rivet points and measured cycle time.
On hand-held equipment, changing rivet size means changing the nosepiece and the feed track. For a dedicated machine, design around your main model and cover the rest with hand-held equipment.
Operation comes down to aim and pull the trigger, so a new operator is productive after a short training session, and the equipment supplier completes that training during on-site installation. For how steep the learning curve is, see how hard is the auto-feed blind rivet machine to operate.
Yes. The manufacturer can bring the machine to your plant, run samples on your actual shells and measure cycle time and appearance on the spot.
Auto-Feed Blind Rivet Machine at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
Antec has served more than 800 sheet metal and enclosure plants with free trials, on-site commissioning, parts supply and maintenance.
Sheet metal plants: try it on your own panels
Send the rivet size and sheet thickness. We will match the auto-feed machine or the pneumatic gun, then run your panels on site before you decide.
5. Cosmetic Parts and Peak-Season Capacity
Appliance makers worry about two things: press marks on cosmetic surfaces and the line stalling in peak season. On appearance, run a batch of samples on your real film-laminated and powder-coated parts before production starts, confirm nosepiece shape, pull force and gun angle, photograph the acceptance standard and file it in the work instruction, and add a protective cap to the nosepiece where needed. On layout, the power unit and rivet bowl usually sit at the line side or hang overhead, hoses run along a balancer arm and the operator's reach stays inside a natural arm radius, which removes wasted motion. On peak-season capacity, auto-feed eliminates the variation that comes from waiting for an operator to pick a rivet, so cycle time becomes predictable and production planning gets easier. The manufacturer provides on-site installation and commissioning, operator training and first-article support worldwide, so the line reaches full takt in the shortest possible time. Complete preventive maintenance and stock wear parts before peak season to avoid a mid-season line stop; the maintenance items are listed in the auto-feed blind rivet machine operation and maintenance guide.
Further reading: how to calculate cycle time and output, hand-held, fixed, dual-gun and robotic cell comparison and auto-feed blind rivet machine
 Previous