You are here:
Automatic Riveting Equipment: Why Rivet Feed Slows in Cabinets - Sheet Metal
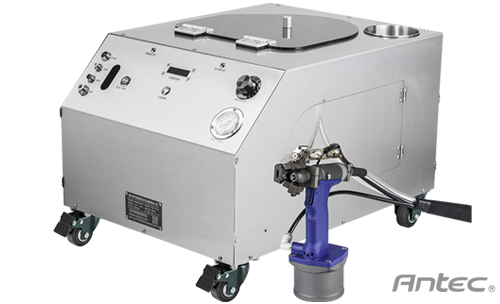
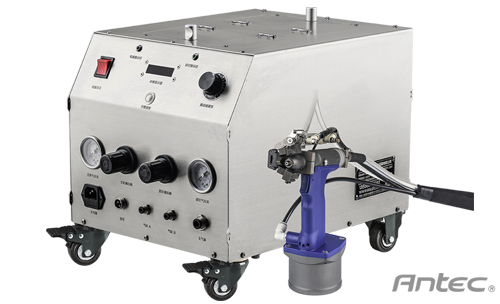
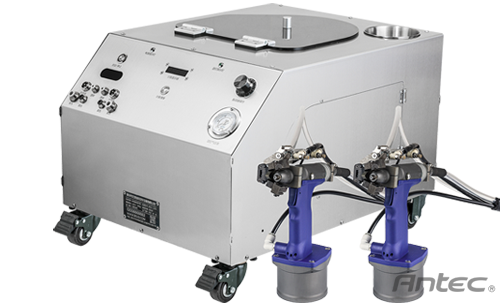
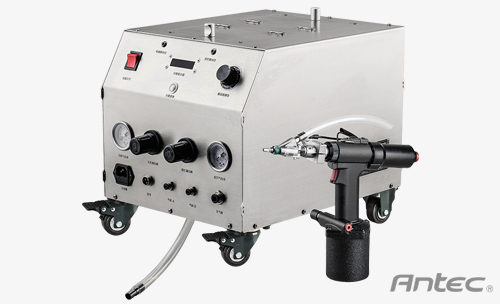
Aluminum extrusion enclosures and electrical cabinets are built in high volumes, and plenty of plants fit an pneumatic rivet gun only to find that rivet feed still feels slow and will not keep up with the line. Using an enclosure and cabinet line as the example, this article shows where the delay really comes from and what to check before blaming the automatic riveting equipment.
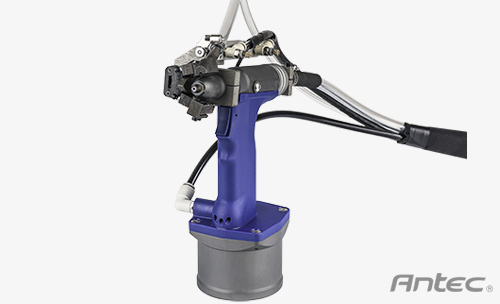
The pneumatic line is what most plants run day to day - smooth feeding, easy air-line maintenance and parts that are always available. Everything below applies to pneumatic rivet gun work in that shop-floor setting.
In short, for sheet metal and enclosure plants: slow rivet feed is not always the gun; line case: automatic riveting equipment on the floor; scratch protection still matters on aluminum cabinets; run a trial before you change equipment.
1. Slow Rivet Feed Is Not Always the Gun
| Symptom | Common cause | What to do |
|---|---|---|
| Frequent rivet jams | Rivet size does not match the feed tube or nosepiece | Match the nosepiece to the rivet size, tidy the feed tube route |
| Feed speed varies | Low air pressure, worn rivet separator | Check supply pressure, replace wear parts |
| Small rivets feed unreliably | Ø2.4–3.2 rivets run in a general-purpose tube | Move to a small-size dedicated feed mechanism |
| Missed rivets and rework | No counting, inspection by eye | Add point counting and an incomplete-cycle alert |
2. Line Case: Automatic Riveting Equipment on the Floor
The plant's existing machines fed rivets unevenly, and missed rivets were common on the night shift. The audit found supply pressure running low and nosepieces that did not match the aluminum rivets in use. After fitting the correct nosepieces, stabilizing air pressure, and switching on counting, the line settled at about 50-60 cycles/min, labor dropped from 4 people to 2, and missed rivets went to zero.
Pneumatic maintenance is simple, but it is not optional - water in the line is the usual culprit.
3. Scratch Protection Still Matters on Aluminum Cabinets
Aluminum extrusion enclosures and powder-coated cabinets have visible faces that show every mark, so specify nylon or chrome-plated scratch-resistant nosepieces and keep stroke pressure under control. For internal threads in door panels, use a rivet nut instead of tapping. Related solutions are on the electronics and electrical: enclosures and cabinets page and under enclosure and cabinet riveting.
4. Run a Trial Before You Change Equipment
Slow feed can start in the air supply, the nosepiece, the rivets, the feed tube, or the operator, and often in more than one place at once. The safest route is to have an engineer bring a machine to your plant and run samples with your own rivets and cabinets, checking each item in turn instead of replacing equipment on a guess.
Shop-Floor Questions
Yes. Fit the small-size dedicated feed mechanism and nosepiece, then run continuously at the trial to confirm the feed does not jam.
In most cases a handheld or in-line machine can be improved with a matching nosepiece, stable air pressure, and a counting module. We assess it on site and quote the work.
Pneumatic Rivet Gun at a glance: 12,800 N pull force, 50-60 rivets per minute, in stock with fast dispatch, on-site commissioning and parts supply.
Parts are held in stock and commissioning is done on site, so the line starts at the rated 50-60 rivets per minute.
Sheet metal plants: try it on your own panels
Send the rivet size and sheet thickness. We will match the auto-feed machine or the pneumatic gun, then run your panels on site before you decide.
 Previous